How to Reduce Risk Between Contract and Go-Live
By DBR77 Team · Published · Updated
Most surprises at start-up were visible months earlier. Between contract and go-live, risk grows when assumptions are never rechecked, changes pile up without decisions, the plant's own tasks slip, and nobody prepares the shift for the first weeks of running the new equipment. You reduce it with three habits: a short risk list reviewed at every milestone, a gate before each phase with checks that must pass, and a production readiness plan that runs in parallel with installation. A small team can run all three if it has dates, owners and the discipline to stop when a check fails.
Why risk grows after the contract is signed
At signature, everyone feels the hard part is done. The supplier is chosen, the price is fixed, the schedule is agreed. Yet many of the project's assumptions have not been tested: the product data, the upstream speed, the network access, the installation window, the people who will run the cell.
During delivery, each of these assumptions meets reality one by one. Most hold. Some do not, and each one that fails late costs more than one that fails early. A wrong product dimension found at the design review means a drawing change. Found at the site acceptance test, it means a new gripper, a lost week and a tense meeting about who pays.
Between contract and go-live, the job is to find failed assumptions as early as possible, while they are still cheap to fix.
Where the risk sits in each phase
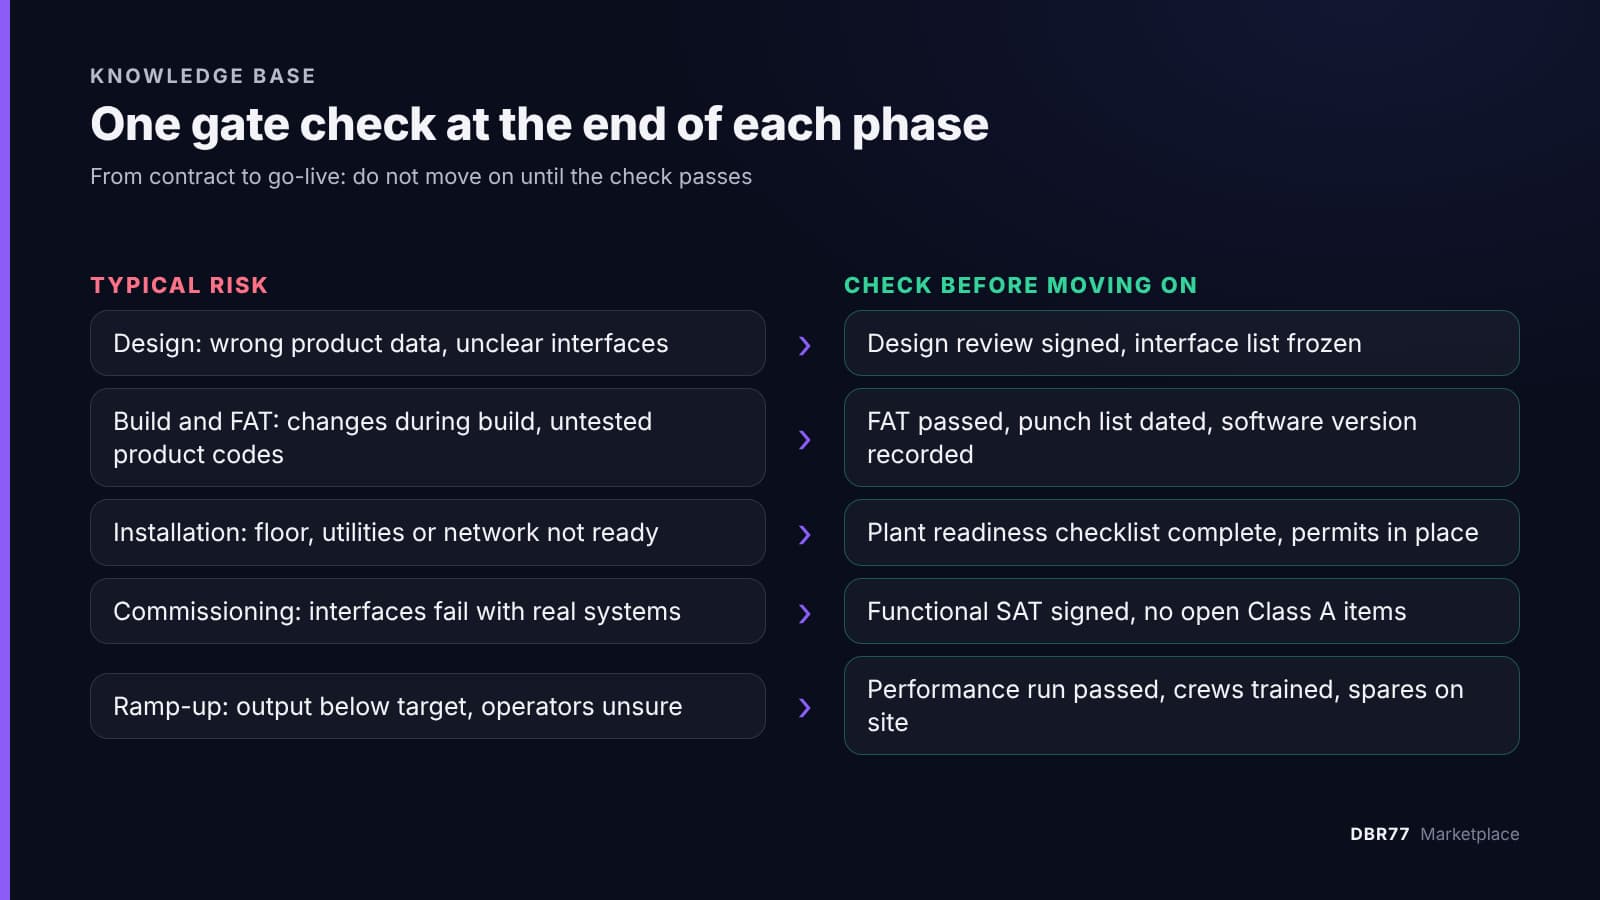
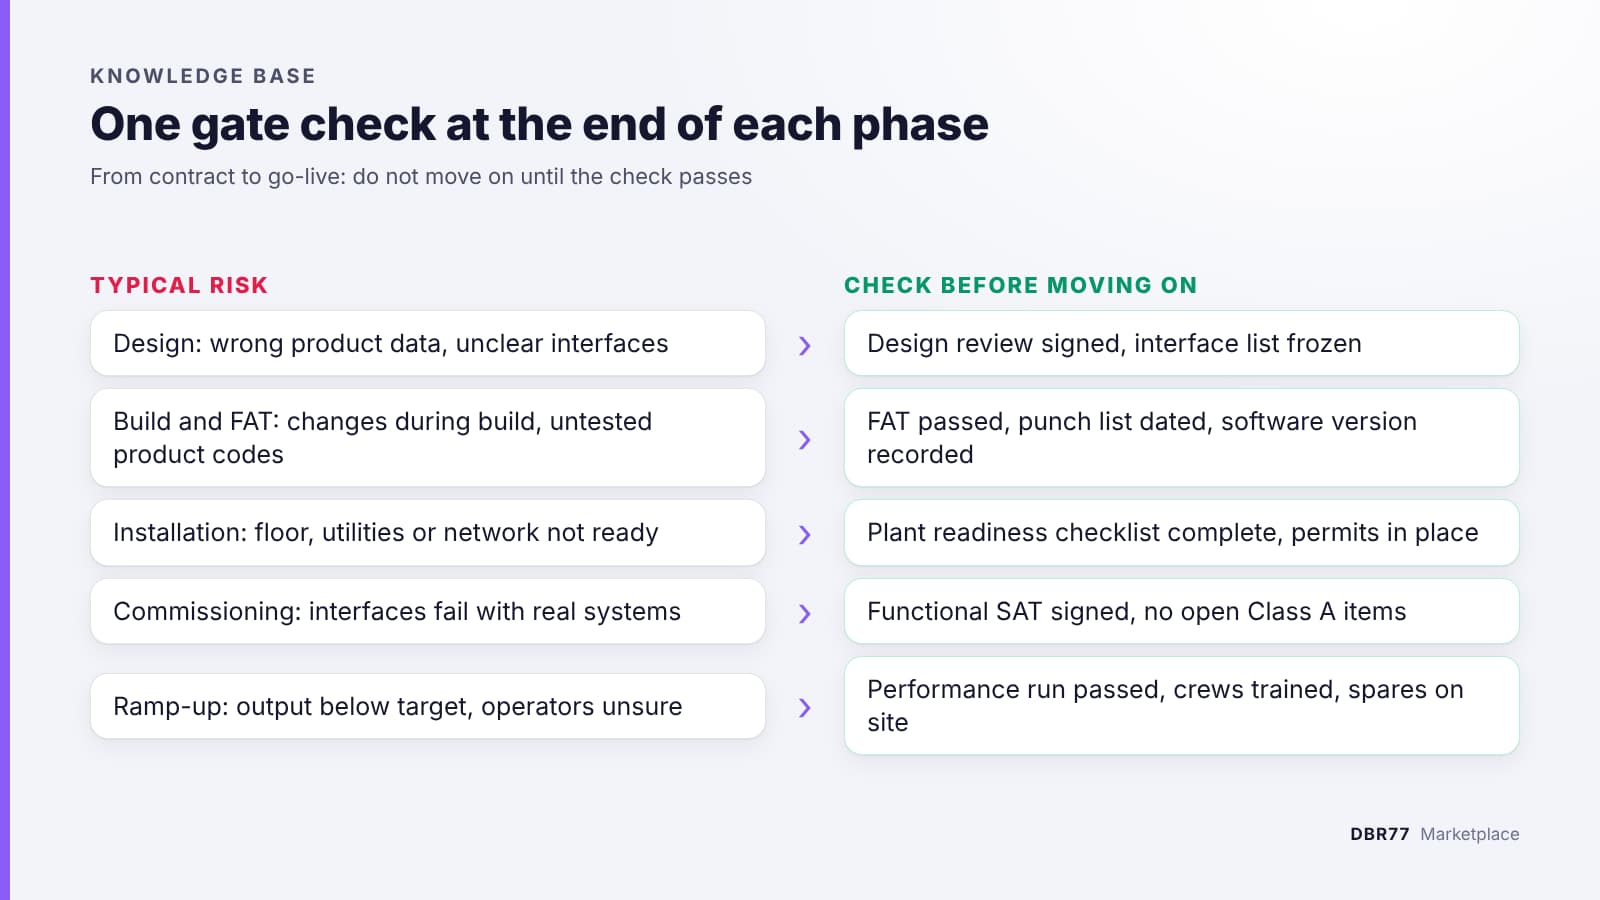
Each phase has its own typical risks and a natural gate at the end. Use the gate to check before moving on.
| Phase | Typical risks | Check before moving on |
|---|---|---|
| Design | Wrong or incomplete product data, layout conflicts, unclear interfaces, safety concept not agreed | Design review signed by engineering, maintenance and safety; interface list frozen |
| Build and FAT | Changes during build, untested product codes, software not finished | FAT passed against criteria; punch list with owners and dates; software version recorded |
| Shipping and installation | Floor, utilities or network not ready; installation window clashes with production; contractor safety | Plant readiness checklist complete; permits and lockout procedures in place |
| Commissioning and SAT | Interfaces fail with real systems, tuning takes longer, tests skipped under time pressure | Functional SAT signed; safety functions verified; no open Class A items |
| Ramp-up | Output below target, operators unsure, maintenance not ready, no backup plan | Performance run passed; trained crews on all shifts; spare parts on site |
To define the FAT and SAT criteria themselves, use How to Set Acceptance Criteria, FAT and SAT for Automation. The handover package and the plant's mobilization plan are covered in From Supplier Selection to Delivery: A Clean Handoff.
Fewer surprises start with a clearer challenge
Describe cycle times, product data and site conditions on DBR77 Marketplace before you ask for offers, so fewer assumptions are left to test later.
How to run a risk review
Keep the risk list short: ten to twenty items is enough for a cell or a small line. For each item write what could go wrong, how likely and how serious it is, who owns it, what is being done and by when. Review it together with the integrator at every gate and at least monthly.
Each review should answer five questions:
- Are we still building what we agreed, or has the scope moved?
- Which assumptions have been verified since the last review, and which are still open?
- Are the acceptance criteria still reachable?
- Are the plant's own tasks on schedule?
- Which new risks have appeared?
End every review with decisions: accept the risk, act on it, or escalate it to the sponsor. Write them down with owner and date.
Ask the integrator to bring its own risks to the review, along with the progress report. Suppliers often see risks early (a late component, an unclear signal list) but wait to raise them until they become problems. An open review gives them a place to do it.
Warning signs of drift
Some signals tell you a project is drifting before the schedule shows it:
- Change requests cluster around one area. Several changes on the same interface or product family usually point to an unclear requirement.
- Plant tasks slip quietly: the network port, the floor marking, the sample parts. Each is small, but together they move the installation date.
- Tests are shortened "to save time". A skipped FAT test is moved to the site, where it costs more.
- Owners stop coming to meetings. When maintenance or IT disappear from the weekly call, their questions will reappear at start-up.
- The integrator's team changes. A new project manager or lead engineer needs the full handover again.
When you see two or more of these at once, hold an extra review. Pausing a week to reset the plan is cheaper than discovering the gap during commissioning. The contract tools for this are the change order procedure, milestones and penalties; for what each should say, read What to Check Before Signing an Automation Contract.
Safety during installation and commissioning
For a robot cell, much of the safety risk sits outside normal production. The OSHA Technical Manual notes that studies in Sweden and Japan found many robot accidents do not occur under normal operating conditions, but during assembly, installation and testing, initial programming, and maintenance. The same chapter says each robot application should have a risk assessment documented before commissioning, and that site acceptance should be performed before initial startup.
In practice, plan for this:
- A risk assessment that covers the installation and commissioning period as well as the finished cell.
- Clear rules for contractor work in a running plant: induction, permit-to-work, marked zones.
- Lockout procedures for the new equipment from the first day of power-on. In the US, the control of hazardous energy is covered by OSHA 29 CFR 1910.147.
- No production runs with safety functions bypassed "just for tonight".
Production readiness: getting the shift ready to run the cell
A cell can pass its tests and still fail in the first month because the plant is not ready to run it. Start this work while the cell is being built:
- People. Name the operators and maintenance technicians for each shift. Plan training before SAT, on the real cell, and check competence afterwards.
- Standard work. Write simple instructions for start-up, changeover, clearing a jam and restarting after a fault.
- Maintenance. Agree the preventive maintenance plan, critical spare parts on site, and the support contact for each shift.
- Cutover plan. Decide when the old process stops. Build a buffer of finished goods or keep a manual fallback for the first weeks.
- Ramp-up target. Agree a realistic curve for the first weeks instead of expecting full output from day one.
Measure ramp-up with data. Output, stops and their causes, logged from the first day, show whether the cell is improving and where to act. If the existing machines are not connected yet, start with The First 30 Days of IoT in a Brownfield Factory.
How DBR77 Marketplace helps
Much of the risk after contract is created before it, through vague requirements and offers based on different assumptions. On DBR77 Marketplace, the Technology Challenge form asks for requirements and operational assumptions, and DBR77 experts review the challenge before it goes live. Integrators who need more detail ask in the Q&A tab, so every bidder works from the same answers.
FAQ
Who should own the risk list, the plant or the integrator?
Both keep their own, but the plant owner should hold one combined list for the project. The integrator owns technical delivery risks. The plant owns its tasks, its people and its production plan.
How often should we review risk?
At every gate (design review, FAT, before installation, SAT, end of ramp-up) and at least monthly in between. On short projects, a weekly ten-minute check of the top five risks is enough.
What if a gate check fails?
Do not move to the next phase. Agree a fix with an owner and a date, and check again. Moving on with a failed check only moves the problem to a more expensive place. If the issue is fundamental, a smaller first phase may have been the better start; How to Run an Automation Pilot or Paid Discovery Phase First explains how to set one up.
Conclusion
Start with the risk list: ten to twenty items, each with an owner and a date, reviewed with the integrator at the next gate. Begin the production readiness plan while the cell is still being built, so operators and maintenance are trained on the real cell before SAT.
Start your next project with fewer unknowns
Post a Technology Challenge with the facts integrators need, or ask our team how it works.
Post your Technology Challenge · Contact the Marketplace team
Sources
- OSHA, OSHA Technical Manual, Section IV, Chapter 4: Industrial Robot Systems and Industrial Robot System Safety, accessed 2026
- OSHA, Control of Hazardous Energy (Lockout/Tagout), accessed 2026